If you’ve ever shopped for CNC equipment for a small to mid-sized job shop, you’ve probably stared down two similar-sounding machines: a CNC drilling tapping machine and a machining center. I get it—when you’re juggling quotes, delivery timelines, and what your shop actually needs to turn a profit, the last thing you want is to mix these two up and end up with a machine that can’t pull its weight. I’ve been selling CNC drilling tapping machines for years now, and I’ve seen way too many shop owners drop a bunch of cash on a machining center when all they really needed was a no-nonsense tapping and drilling rig, or vice versa. Let’s break this down like we’re sitting at a coffee shop after a long day on the floor, no fancy engineering jargon to make your head spin. CNC Drilling Tapping Machine
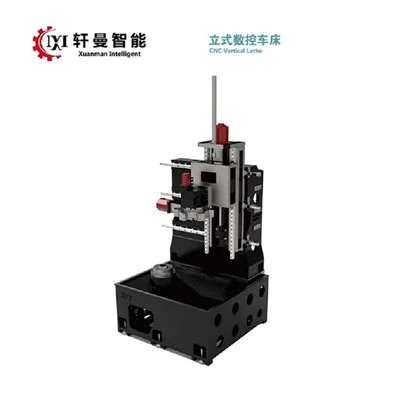
First, let’s start with the basics that most people gloss over. A CNC drilling tapping machine, at its core, is built for one very specific job: drilling holes and tapping threads into them. That’s it (well, almost it). It’s not meant to do a million other things, and that’s exactly why it works so well for the work a lot of shops do day in and day out. When I show a new machine to a customer, I start by saying, “If you’re making brackets, fasteners, small engine parts, or any part that just needs a few holes and threads, this is your go-to.” It’s got a rigid spindle that’s built to handle the thrust of drilling through metal, plastic, or even hardwood, and the tapping function is tuned to be smooth and consistent—no stripped threads, no broken taps, which is a huge win for small batches or high-volume runs where rework kills your margin.
A machining center, though? That’s the overachiever cousin. It’s got way more axes, usually three or more (sometimes four or five, if you’re splurging), and a full automatic tool changer (ATC) that can hold anywhere from 10 to 100 tools. So where a drilling tapping machine would need you to manually swap out a drill bit for a tap, a machining center just swaps the tool all on its own. That means it can drill, tap, mill, face, contour—you name it, it can do it. If you’re making a complex part that needs to have a curved surface milled, or a pocket cut out, or multiple different operations in one setup, a machining center is the way to go. But here’s the thing: that extra capability comes with extra cost, extra space, and extra downtime if you’re not using all those tools.
Let’s talk about size and setup, because that’s a big one for most shops. CNC drilling tapping machines are compact, for the most part. Most models fit on a 5×5 ft or 6×6 ft table, so you don’t need to clear out a whole corner of your shop to fit it. They’re also lightweight compared to machining centers, so shipping and installation are way cheaper and faster. I’ve had customers take delivery of a drilling tapping machine in the morning, have it leveled and programmed by lunch, and be running parts by the end of the day. Machining centers, on the other hand, are bulkier. A 3-axis vertical machining center (VMC) will take up 8×8 ft or more of floor space, and larger ones need a reinforced concrete base because they’re heavy enough to shift if you don’t anchor them right. Installation takes days, sometimes weeks, because you have to level it perfectly and set up the ATC and coolant system, plus run a custom power line if it needs more juice. That’s not a big deal if you’re doing complex parts, but if you just need to drill and tap, that’s extra hassle you don’t need.
Next up, accuracy and speed—two things every shop cares about, but they play different roles here. People always assume machining centers are more accurate, but that’s not exactly true for the jobs both machines do. CNC drilling tapping machines are precision-built for their specific tasks. Their spindles spin at high RPM (often 10,000 to 30,000 RPM, sometimes higher) to get clean, fast holes, and the tapping cycle is calibrated to reverse at the exact right moment to avoid breaking taps or leaving messy threads. For small, tight-tolerance parts—like a bracket with 10 holes needing ±0.001 inch accuracy—my drilling tapping machines can hang with almost any machining center, because they don’t have extra moving parts to introduce error. The only place they fall short is when you need to mill a shape or cut a contour, which is where machining centers shine.
Machining centers, though, are built for multi-axis movement, so their accuracy holds up when you’re moving a tool along a curved path or at an angle. But because they have that big tool changer and a longer travel range (sometimes 40 inches or more on the X-axis, vs. 12 to 20 inches on a standard drilling tapping machine), they have more parts that can wear over time. That means if you’re running a high-volume tapping job for months on end, a drilling tapping machine will keep its accuracy longer than a machining center that’s only used for tapping. The machining center is a jack of all trades, so it’s good at everything, but master of none—at least when it comes to drilling and tapping.
Cost is probably the biggest difference most people care about, and it’s not even close. A new CNC drilling tapping machine will set you back anywhere from $15,000 to $50,000, depending on the size, spindle speed, and features you need. A used one might be even cheaper, around $5,000 to $20,000, if you’re on a tight budget. Machining centers? Entry-level 3-axis VMCs start at around $50,000, and mid-range models can go for $100,000 or more. If you get into 4 or 5-axis machining centers, you’re looking at $150,000 and up. That’s a huge gap, and it’s not just the sticker price—operating costs are lower too. Drilling tapping machines use less power, since their spindles are smaller, and they don’t need as many cutting tools or coolant, because you’re only using two or three tools per job instead of a dozen. I’ve had a customer tell me that for their small engine bracket runs, their drilling tapping machine cuts part costs by 30% compared to using a machining center, because they don’t have to pay for extra setup time and tool wear on the more expensive machine.
Flexibility is where the machining center wins, but it’s a double-edged sword. If you’re a job shop that gets a mix of simple drilling/tapping jobs and complex milling jobs, a machining center can do both, so you don’t need two machines. But if 80% of your work is just drilling and tapping, that extra flexibility is wasted. You’re paying for tools you’ll never use, axes that will never move beyond linear travel, and setup time that adds up because you’re always switching between jobs that need different tooling. I had a customer last year who bought a used machining center thinking it would handle everything, but after six months he realized he only used 2 out of 15 tools in the ATC. He sold the machining center and picked up two of my drilling tapping machines, one for small parts and one for larger ones, and his throughput went up by 40% because he didn’t have to wait for tool changes or setups.
Wait, let’s talk about tooling and setup, because that’s another pain point. For a drilling tapping machine, you don’t need a fancy tool changer. You just change out the drill bit and tap manually—most jobs only need two tools, so it takes 30 seconds or less. Setup time is super fast: you load the program, clamp the part, and hit run. For high-volume jobs, you can even add a parts feeder to automate loading, so it runs 24/7 with minimal supervision. Machining centers need way more tooling—each operation needs a separate tool, so you have to pre-load tools into the ATC, which takes time and adds cost. Setup takes longer too, because you have to set tool offsets, test each tool path, and make sure there’s no tool collision. That’s fine for a complex job that needs multiple operations, but for a simple drilling and tapping job, it’s a total waste of time.
Also, let’s not forget about maintenance. CNC drilling tapping machines are simpler, so there’s less that can go wrong. The spindle is smaller, the moving axes are fewer, and there’s no ATC to jam. Most maintenance is just regular cleaning, changing the oil, and checking the tool holders—stuff that takes 30 minutes a week, not hours. Machining centers have more parts to service: the ATC needs lubrication, the linear guides need more frequent checks, and the spindle is bigger so it needs more maintenance to keep it accurate. I’ve had customers tell me that their machining center’s maintenance costs are twice as much as their drilling tapping machine’s, just because of all the extra parts.
Now, I know what you’re thinking: “What if I might need to do milling someday?” That’s a fair question. If you’re a small shop that’s just starting out, or you mostly do simple parts, a drilling tapping machine is a way better investment. You can always upgrade later if you need to add a milling function, or buy a machining center when your workload grows. If you buy a machining center first when you only need drilling and tapping, you’re tying up cash that you could use for materials, marketing, or hiring more help. I always tell new customers to ask themselves one question: “What percentage of my jobs require operations other than drilling and tapping?” If it’s less than 50%, go with a drilling tapping machine. If it’s more than that, then a machining center makes sense.
Let me give you a real example. Last month, I worked with a customer who makes custom metal brackets for the construction industry. Every bracket needs 4 to 6 holes, each with a thread, and that’s it. He had a machining center that he’d bought years ago, thinking he’d branch out into other parts, but all his work was these brackets. He was spending $80 an hour on the machining center, even though most jobs took 15 minutes, because of setup and tool changes. We sold him two of our entry-level CNC drilling tapping machines, and now each bracket takes 5 minutes to run, with setup time cut in half. His labor costs went way down, and he could take on more jobs because he could run parts faster without tying up the big machining center.
Another customer is a job shop that does a mix of simple brackets and custom automotive parts that need milling pockets. He has both: one machining center for the complex jobs, and two drilling tapping machines for the high-volume simple jobs. That’s the sweet spot, right? You use each machine for what it’s best at, instead of forcing one machine to do everything. You get the accuracy and speed you need for drilling and tapping, and the flexibility for when you need to do more complex work.
So to wrap this up, let’s cut through the noise and sum up the key differences, no fancy charts or terms. A CNC drilling tapping machine is a specialized workhorse built for fast, accurate, consistent drilling and tapping. It’s compact, cheap to buy and run, easy to set up, and perfect for high-volume or simple jobs where you don’t need extra operations. A machining center is a versatile multi-tool that can do drilling, tapping, milling, and more, but it’s bulkier, more expensive, harder to set up, and overkill for most drilling and tapping work.
If you’re tired of paying for capabilities you don’t need, or if you’re looking to upgrade from manual drilling and tapping that’s slow and inconsistent, a CNC drilling tapping machine is probably the right call for your shop. It’s not going to do contour milling or 5-axis work, but it will make the parts you need to make, faster and cheaper than any machining center can. If you’re ready to stop wasting money on overkill equipment and start running your parts more efficiently, I’m here to help. We can walk through your workload, figure out what size and features you need, and get you set up with a machine that actually works for your bottom line. Don’t just take my word for it—talk to other shop owners who’ve made the switch, and you’ll hear the same thing: a drilling tapping machine is the unsung workhorse that keeps small shops profitable.

Now that you have a clearer picture, if you’re ready to find the right CNC drilling tapping machine for your operations, feel free to reach out for a chat about your specific needs. We can go over everything from part sizes to production volumes to make sure you get exactly what you need without overspending.
CNC Turning Machine References
- Machine Technology: Principles and Practice, 2nd Edition
- Modern Machining Technology, 5th Edition
- CNC Machining Fundamentals: A Practical Guide for Operators and Programmers
- Global CNC Machine Market Report, 2023
Jiangsu Xuanman Intelligent Equipment Co., Ltd.
As one of the most professional CNC drilling tapping machine manufacturers in China, we’re featured by quality products and low price. Please rest assured to buy discount CNC drilling tapping machine made in China here from our factory. Customized orders are welcome.
Address: No.1-1, Weier Road, Jieji Equipment Manufacturing Industrial Park, Sihong County, Suqian City, Jiangsu Province, China
E-mail: jsxmzn@163.com
WebSite: https://www.xm-machs.com/
